InSight Software
Unlock the power of connected equipment for peak factory performance.
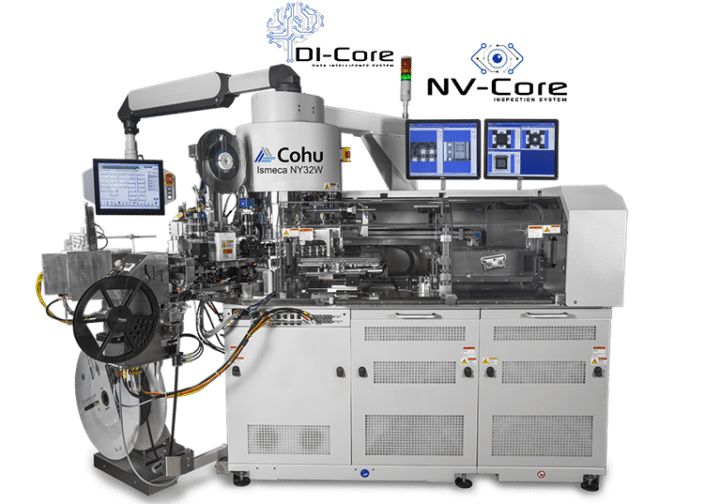
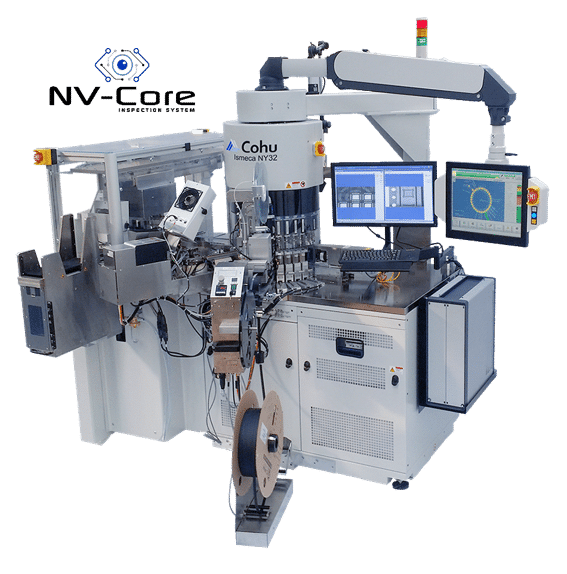
Cohu’s InSight™ factory monitoring and control software empowers semiconductor manufacturers with real-time visibility, centralized control, and actionable insights across their test handler and inspection equipment. Designed to drive efficiency, reduce downtime, and enable data-driven decisions, this solution helps teams maintain peak performance in high-volume, high-precision environments. From remote access and KPI tracking to predictive maintenance and centralized data management, it’s a foundational step toward a smarter, more connected factory.
Keep your production running smoothly from anywhere on the factory floor—or beyond. Operators and engineers can remotely monitor and control semiconductor test handler and inspection systems directly from the factory control room. This capability enhances operational flexibility, accelerates issue resolution, and reduces dependence on on-site intervention during high-volume production.
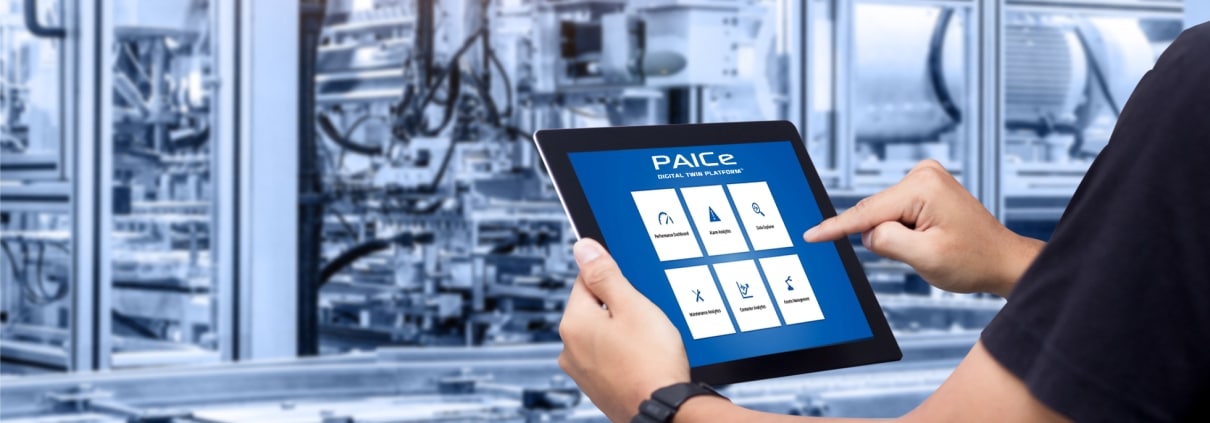
Track what matters most. Continuously monitor critical performance indicators—including Overall Equipment Effectiveness (OEE), Units Per Hour (UPH), yield, test time, and failure statistics. Real-time intuitive dashboards provide visibility and actionable insights that support data-driven process improvements and faster decision-making.
Stay ahead of downtime. Integrated preventative maintenance scheduling, alarm handling, and recipe management tools reduce unplanned downtime and ensure equipment consistency. These functions enable predictive responses to performance drifts or process anomalies, supporting higher system availability and sustained output quality.
Enable faster troubleshooting and better decision-making. All equipment parameters, alarms, performance metrics, and recipes are captured and stored in a centralized knowledge database. This structured data foundation supports historical analysis, process bench-marking, and cross-tool learning across the fleet—advancing the factory’s Industry 4.0 readiness.
Complete our contact form.